Oct 02, 2026
Last Updated: 2 October 2026
Bridge manufacturing is the practice of producing a limited run of parts using a fast, tooling-free method so you can launch, sell and gather feedback while slower mass-production tooling is prepared. For electronics design, it closes the gap between a working prototype and full-scale output.
At 76 ADDITIVE in Ely, we see this shift constantly. Startups and SMEs come to us with a validated design and a problem: they need sellable units now, not in six months. Bridge manufacturing solves that.
It is not a stopgap you tolerate. It is a deliberate stage in your production plan.
Traditional tooling means committing to hard steel moulds before you know if the market wants your product. That is a large, risky spend.
Bridge manufacturing flips the order. You produce real, end-use parts first, then invest in tooling once demand is proven.
Factor | Traditional Tooling | Bridge Manufacturing |
|---|---|---|
Upfront cost | High, paid before launch | Low, pay per part |
Lead time to first units | Long | Days, not months |
Design changes | Expensive to make | Cheap to make |
Best for | Proven, stable designs | New or evolving products |
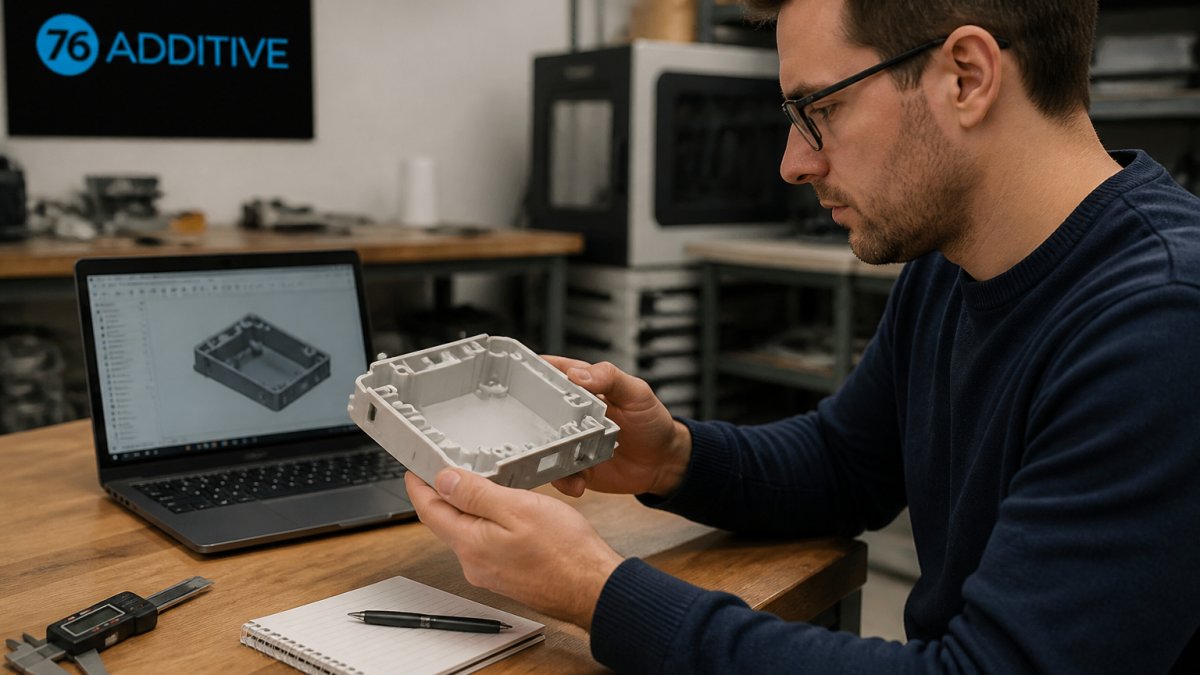
The trade-off is unit cost. Bridge parts cost more per piece than moulded parts at high volume. But at low volume, the maths usually favours bridge production because you avoid the tooling bill entirely.
Three distinct bridges show up in electronics work, and each solves a different problem.
A tooling bridge covers the wait for your injection moulds. You make parts with additive manufacturing while the mould is cut, so your launch is not delayed.
A production bridge is a full low-volume run made without tooling. It is ideal when you need hundreds of units and the design may still change.
A supply chain bridge keeps you covered when a supplier falters or a component is delayed. You print the part locally instead of waiting on a shipment.
The methods behind bridge production are additive: parts are built layer by layer from a digital file, so no mould is needed.
Two processes dominate for end-use electronics parts. Multi Jet Fusion (MJF) makes strong, consistent nylon parts with fine detail. Carbon DLS uses a resin process for smooth surfaces and tight tolerances (DLS 3D Printing Technology).
Both suit enclosures, brackets, connectors and internal housings. The key point is repeatability. You need every batch to match the last one.
That consistency is what lets a bridge run stand in for a moulded part. If the process drifts, the parts fail.
Rapid tooling for electronics design means creating the tools or parts you need in days rather than months. It fits best when speed to market matters more than the lowest possible unit cost.
Use it when you are testing a new product, when your volumes are uncertain, or when a design change is likely. It also works well for custom or low-run products where a mould would never pay for itself.
What most guides miss is that rapid tooling is not just for prototypes. It produces parts that go into products people buy. The line between prototype and production has blurred.
Low-volume electronics manufacturing in the UK changes the moment you move past a handful of units. At 500 to 2,000 units per run, you need repeatable quality, not one-off parts.
This is the sweet spot for bridge manufacturing. You are past prototype stage but not yet at the volumes that justify hard tooling.
At this scale, additive manufacturing keeps your options open. You can adjust the design between runs without scrapping a mould. You can hold digital inventory and print to order.
The practical shift is in planning. You stop thinking in single batches and start thinking in repeatable runs. That means documented settings, consistent material and a partner who can match the last batch exactly.
Pick a partner on repeatability, communication and scale, not on the lowest quote. A cheap part that fails in the field costs far more than a reliable one.
Look for direct access to the people running the machines. You want to talk to the operator, not a call centre. That conversation is where tolerance questions get answered honestly.
For anyone searching for bridge manufacturing near me, the answer is often closer than expected. Ely sits within easy reach of the region's advanced manufacturing cluster.
The biggest mistake is treating bridge production as a temporary fix rather than a real production stage. Teams rush it, skip documentation and then cannot repeat the result.
A second error is over-investing in tooling too early. If you cut steel before demand is proven, you carry the risk of a design you cannot change. Start with additive, prove the market, then tool up.
A third is choosing a supplier on price alone. Consistency is worth more than a small saving per part. Parts that fail in the field cost you customers.
Getting sellable electronics to market without a huge tooling bill is the challenge every hardware founder faces. Bridge manufacturing answers it, and 76 ADDITIVE is built for exactly this stage.
We offer state-of-the-art MJF and Carbon DLS 3D printing, no tooling investment required, and direct communication with the operator running your parts. With 17 years in design and manufacturing, we produce high-quality, repeatable end-use components for low and mid-size runs.
Get started with 76 ADDITIVE and move from prototype to production without the tooling gamble. Request an instant quote today.
Bridge manufacturing is the stage between prototyping and full-scale production. It lets you make end-use parts in low to mid volumes without committing to expensive injection moulding tooling. For electronics design, this means you can get functional housings, brackets, and enclosures into customers' hands while your design is still being refined. If your product changes, you adjust the digital file rather than scrapping a mould. It reduces the risk of tooling a design that is not quite right yet.
Move to bridge manufacturing when your design is stable enough for real-world testing but you are not ready for mass production volumes. Typical triggers include securing your first paying customers, needing to fulfil a pilot order of 500 to 2,000 units, or preparing for a funding round that requires demonstrable market traction. At this stage, additive manufacturing gives you production-quality parts without the lead time and cost of traditional tooling. You can still make design tweaks between batches if feedback demands it.
Traditional tooling for injection moulding can take weeks or months to cut and validate. Bridge manufacturing skips that step entirely by printing end-use parts directly from digital files. You can go from final design to shipped product in days rather than months. That speed matters when you are trying to hit a trade show, fulfil a pre-order campaign, or get ahead of a competitor. It also lets you iterate faster because you are not waiting on a third-party toolmaker for every revision.
The main saving is avoiding tooling investment altogether. Traditional injection moulding requires a steel or aluminium mould that can cost thousands of pounds before you produce a single part. Bridge manufacturing using additive processes eliminates that upfront cost. Your per-part price may be higher than mass-produced moulded parts, but at volumes under 2,000 units the total spend is often lower because you are not amortising tooling across a small batch. You also avoid the cost of re-tooling if your design changes.
Opening Hours (our printers run through the night)
Monday - Friday, 9am - 5pm


76 Additive
19 Hall Barn Road Industrial Estate
Isleham, Ely
Cambridgeshire, CB7 5RJ
76 Projects t/a 76 Additive
Registered in England & Wales Company no: 10235633
VAT: 245 830 796