Sep 30, 2026
Last Updated: September 30, 2026
Rapid iteration for product design is the practice of shortening the loop between concept, physical part and tested result so each design decision is based on evidence rather than assumption. At 76 ADDITIVE, we've spent 17 years in design and manufacturing, and the pattern is consistent: teams that shorten that loop learn faster than teams that spend longer perfecting a single design before testing it.
The old model held that you design, tool up and produce. That works when a design is stable and volumes are high. It falls apart when a product is still evolving, because every change means re-cutting steel. Rapid iteration replaces the tool with a direct digital-to-part workflow, so a revised CAD file becomes a physical component in days rather than months.
That shift matters most for startups and SMEs working in Ely and across the wider region, where capital for tooling is limited and the cost of being wrong is high. The core argument of this guide is simple: iteration speed is now a competitive advantage in its own right, and additive manufacturing is what makes it affordable at low and mid-size volumes.
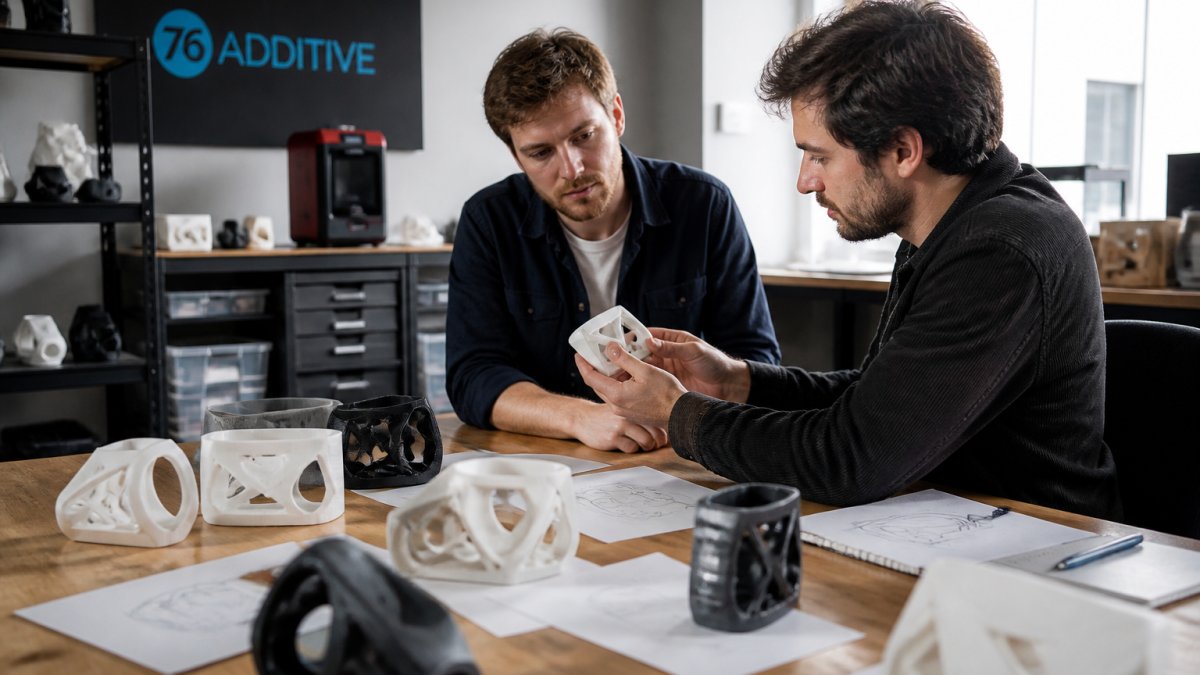
Rapid prototyping produces a model to look at. Rapid iteration produces a functional part to test, measure and improve, then repeats the cycle until the design is proven.
The distinction is not semantic. A prototype confirms a shape; an iteration tests a decision. When you print a bracket to check it fits, that is prototyping. When you print that bracket in the production material, load it to failure, adjust the wall thickness and print again, you are iterating. The output of the second process is data, not a model.
Most guides treat prototyping as the end goal. It isn't. Prototyping is one step inside a loop, and the loop is what delivers a manufacturable product.
For most small-batch production, yes, provided you understand where the money goes. The break-even point is not about unit price alone; it is about whether you can absorb the cost of tooling before you have proven demand.
Injection moulding spreads a large fixed tooling cost across every part. At high volumes that cost becomes negligible. At 500 to 2,000 units per run, it dominates. Additive manufacturing removes the tool entirely, so the cost per part reflects machine time and material rather than amortised steel. You pay more per unit and less to start.
That trade favours anyone who is still learning. If your design will change after the first production run, tooling is money spent on a version you are about to replace.
Tooling costs bite in three places that rarely appear in a simple quote. First, the initial tool itself, which you pay for before a single saleable part exists. Second, design changes: a modification to a moulded part often means modifying or remaking the tool. Third, the delay. Every week spent waiting for a tool is a week your product is not in customers' hands and not generating feedback.
For a startup, that third cost is the one that hurts. A tool that takes weeks to cut does not just cost money; it freezes your design at the moment you knew least about it. By the time parts arrive, your thinking has moved on and the tool is already obsolete.
Additive manufacturing removes the first two costs and collapses the third. A revised file can be printed the same week it is approved, which means your design keeps improving right up to the point of production.
Reducing time-to-market for physical products comes down to removing the waiting steps between a design decision and a tested part. Most of the elapsed time in a traditional programme is not design work; it is queueing for tooling, shipping samples and waiting for a batch to come back before you can test it.
Compress those gaps and the whole programme accelerates. A team that can hold a physical part within days of a CAD change will run more test cycles in a quarter than a team waiting on tooling runs in a year. More cycles means more problems found early, when they are cheap to fix.
The practical levers are straightforward:
3D printing for end-use components changes the assumptions you can make about what a printed part is for. A printed component is no longer a stand-in for the "real" part; it is the real part, produced without a tool and repeatable across batches.
That shift has three practical consequences. Design freedom increases, because processes that build a part layer by layer can produce internal channels and integrated geometries that moulding cannot. Inventory becomes digital: you hold a file rather than a shelf of parts, and print to demand. And revision becomes cheap, because a design change is a file change, not a tool change.
The question buyers ask most often is whether additive can hold the tolerances their application demands. For demanding sectors such as aerospace and automotive, that is the right question to ask. It is answered by process selection and by running a small test batch against your actual specification before committing to volume, not by taking a supplier's word for it.
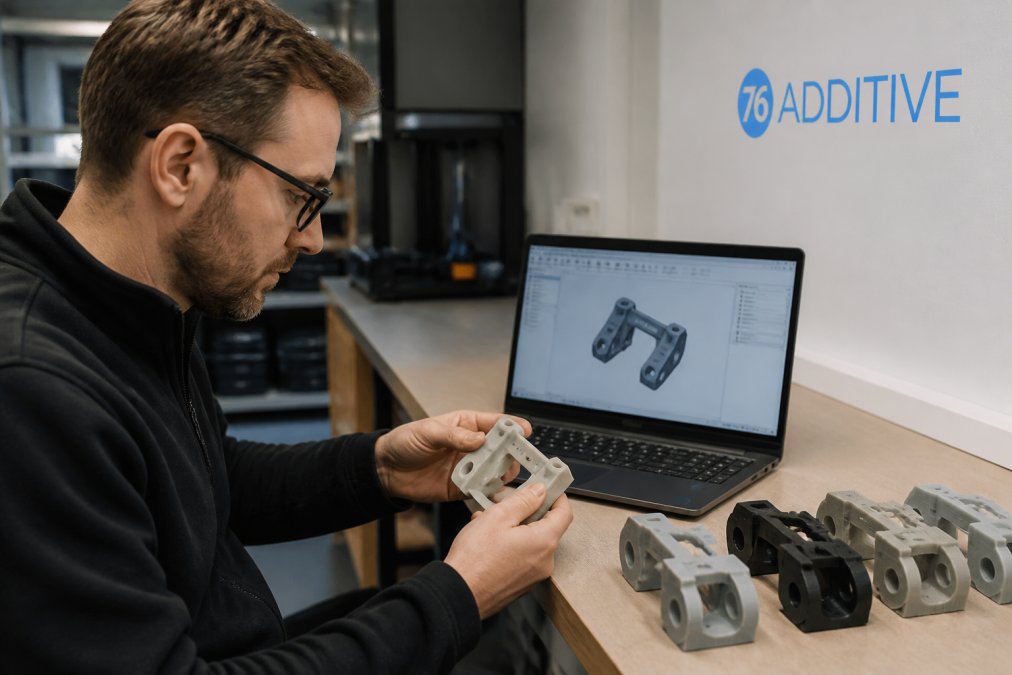
The iteration cycle has four stages, and the discipline is in not skipping any of them. Design the change, print the part, test it against a defined measure, then refine based on what the test showed. Each full turn of the loop should answer one question.
Total time per cycle: days, not weeks, once the workflow is established.
What you'll need before you start:
Then work the loop:
Most teams find the first cycle slow and the later ones fast, because the workflow and the test rig are already built.
Over-engineering the first design is the biggest time sink. Teams spend weeks perfecting a part before it has ever been tested, then discover the constraint they optimised for was not the one that mattered.
Other frequent slowdowns:
A common mistake is to treat additive as a prototyping-only tool and then re-tool for production. If the part is going to be printed in production anyway, test it that way from the start.
The real challenge in physical product development is not having good ideas; it is proving them quickly enough to act on them before the market moves. Every week spent waiting on tooling is a week your competitors spend testing.
76 ADDITIVE exists to remove that wait.
Rapid prototyping is the act of producing a physical model quickly, usually to check form or fit. Rapid iteration is the repeated cycle of design, print, test and refine that uses those prototypes to improve the product. One is a single output; the other is a process. Teams that treat prototyping as a one-off often stall, while those running a structured rapid iteration loop catch design flaws earlier and reach a manufacturable version with fewer costly changes.
For runs of roughly 500 to 2,000 units, additive manufacturing often avoids the upfront tooling spend that traditional injection moulding demands. That means you can validate the design, gather customer feedback and adjust before committing to hard tooling. The trade-off is unit cost at very high volumes, where moulding still wins. For small batches, the flexibility and lower financial risk usually outweigh the per-part difference.
Most cost is locked in once tooling is cut. If a design flaw surfaces after that point, you pay for new moulds and lost production time. Rapid iteration lets you test fit, function and tolerances on printed parts first, so changes happen while they are still cheap. Startups also avoid holding large inventories, since parts can be produced on demand as orders come in rather than in a single large tooling run.
It depends on the process and the material. Industrial methods such as Multi Jet Fusion and Carbon DLS are used for production parts in sectors where repeatability matters, including cycling and automotive applications. Tolerances are tighter than many people expect from desktop printing, but they are not identical to machined metal. The sensible approach is to run a small test batch first and measure the results against your specification before committing to a larger order.
Opening Hours (our printers run through the night)
Monday - Friday, 9am - 5pm


76 Additive
19 Hall Barn Road Industrial Estate
Isleham, Ely
Cambridgeshire, CB7 5RJ
76 Projects t/a 76 Additive
Registered in England & Wales Company no: 10235633
VAT: 245 830 796