Oct 18, 2026
Last Updated: 17 October 2026
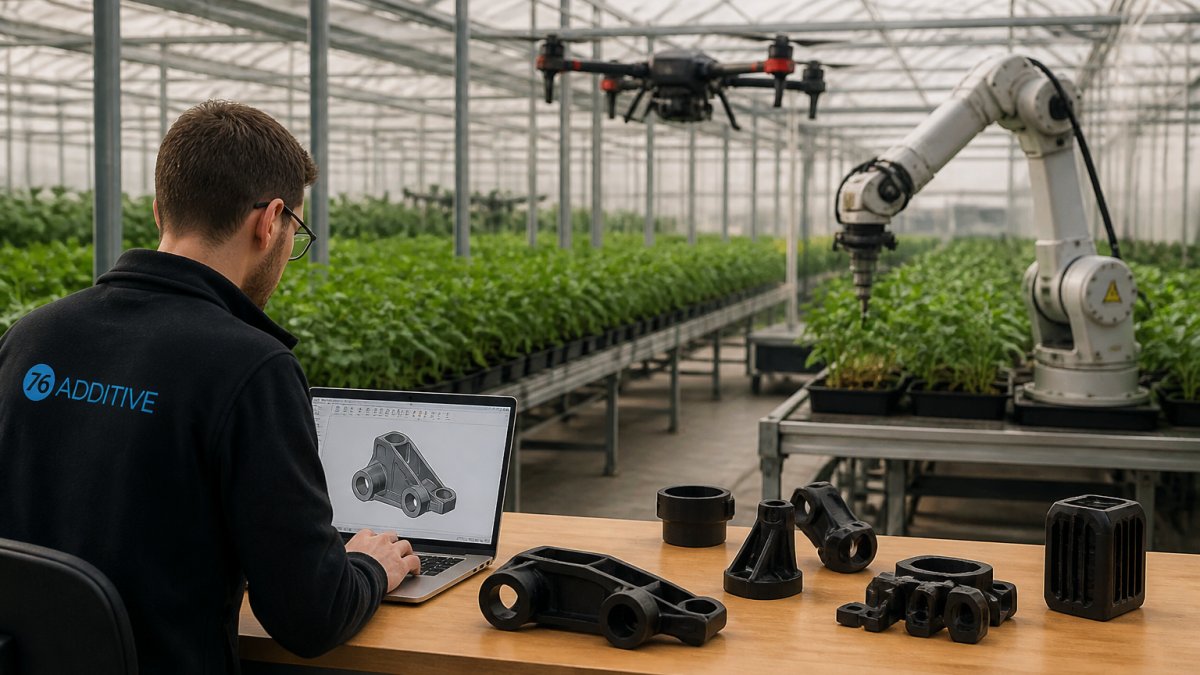
Additive manufacturing for agritech design is the use of layer-by-layer 3D printing to produce parts for agricultural machinery, sensors and field equipment, and it fits because farm kit is low-volume, highly varied and punishing to use. At 76 ADDITIVE in Ely, Cambridgeshire, we have spent 17 years in design and manufacturing, and we see the same pattern repeat: agritech teams need tough parts in small numbers, fast. Traditional tooling cannot move at that pace. Printing can.
Three forces make printed parts a natural fit:
That is the theory. Here is what it means in practice.
3D printing for agriculture earns its place where parts are low-volume, geometrically awkward or needed quickly for field trials. It is not a replacement for every moulded component. It is the right tool for a specific job.
The parts that work best share a few traits. They are produced in modest numbers, they carry real load or exposure, and their shape would be costly to tool.
| Component | Why printing suits it | Typical material |
|---|---|---|
| Sensor housings | Sealed, complex internal geometry | Nylon PA12 |
| Mounting brackets | Custom fit to existing frames | Glass-filled nylon |
| Nozzle and sprayer parts | Internal channels, small batches | Rigid engineering plastic |
| Drone components | Lightweight, integrated shapes | Carbon-fibre reinforced |
| Replacement knobs and clips | Low volume, fast turnaround | Tough nylon |
A common mistake is printing a part that should be moulded. If you need tens of thousands of identical pieces, tooling usually wins on unit cost. Below that, printing often wins on total cost and speed.
Design for additive manufacturing is the practice of shaping a part around how a printer builds it, and following a few rules saves you reprints. Ignore them and you burn time and money on failed builds.
The rules that matter most for agritech parts:
Wall thickness decides how a part behaves under vibration. Radii decide whether it cracks at a corner. Orientation decides whether it prints cleanly at all.
A simple workflow keeps iterations low:
We would rather spend an hour on the model than a day on a reprint.
Agricultural equipment prototyping without tooling means testing real, functional parts before anyone pays for a mould. That is the single biggest cost saving in the whole process.
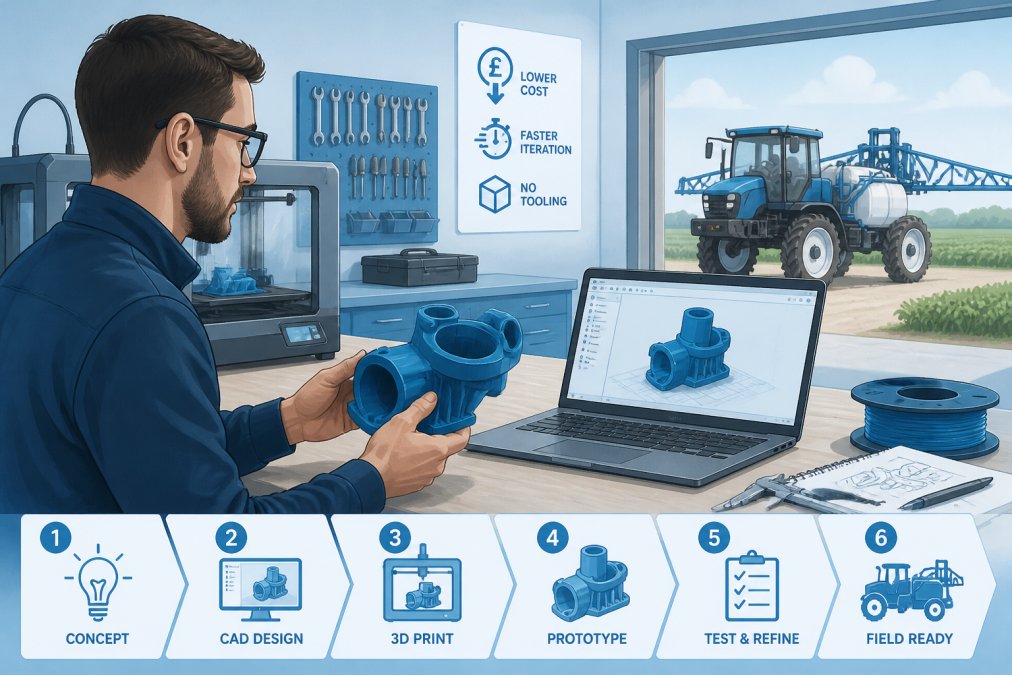
No tooling means you can change the design between builds. A bracket that fouls a frame gets fixed in the model, not in a workshop. A housing that traps mud gets a new drain path in an afternoon.
The iteration loop is short:
Most teams get through several rounds in the time a mould would take to arrive. You can contact our team to talk through a first test batch.
Material choice decides whether a part lasts a season or a decade. Agritech parts face mud, sunlight, pressure washing and chemical spray, so the plastic has to earn its place.
The main options we work with:
Match the material to the exposure. A part that lives outdoors needs UV stability. A part that gets washed down needs to handle moisture without swelling or cracking. A part on a drone needs to be light without going brittle.
What most guides miss is that the finish matters as much as the plastic. Sealing or coating a printed part can extend its life outdoors considerably. We advise on this per part, because there is no single answer.
Low-volume manufacturing for agritech beats moulding when tooling cost and lead time outweigh the per-part saving. For runs in the hundreds or low thousands, printing is often the cheaper route to market.
Here is how we would decide:
| Your situation | Better route |
|---|---|
| Under a few hundred units | Additive manufacturing |
| Design still changing | Additive manufacturing |
| Complex internal geometry | Additive manufacturing |
| Tens of thousands, design frozen | Traditional moulding |
The break-even point sits where tooling cost divided by unit volume stops being worth it. Below that line, printing wins. Above it, moulding usually does.
There is a second benefit that rarely gets mentioned: digital inventory. With no mould and no minimum run, you can hold a digital file and print replacement parts on demand. That suits agritech well, where a machine breakdown mid-season is costly.
If you are weighing up a first production run, an instant quote will tell you where you stand.
The real challenge in agritech is not designing a part that works once, but one that survives seasons of mud, sun and vibration without a costly mould behind it. That is where additive manufacturing earns its keep, and it is where we can help. At 76 ADDITIVE in Ely, we offer MJF and Carbon DLS printing with no tooling investment, direct contact with the operator and end-to-end design support. Get started with 76 ADDITIVE and move from prototype to field-ready parts faster.
It depends on the material and the load case. Printed nylon parts handle UV exposure, mud and routine washdown well when they are designed with adequate wall thickness and the right print orientation. For parts that see heavy impact or constant abrasion, choose a tougher grade and test a small batch in the field before committing to a full run. Bring 76 ADDITIVE your operating conditions and they will recommend a material and build orientation that suits them. A short field trial settles the question faster than any datasheet.
For runs of roughly 500 to 2,000 units, printed production often works out cheaper than committing to injection moulding tooling, because there is no tooling investment to recover. The crossover point depends on part size, material and how much finishing the part needs. Below a few hundred units the case is strong; above a few thousand, moulding starts to win on unit price. 76 ADDITIVE can quote both scenarios so you can see where the break-even sits for your part.
Start by removing features that only exist because moulding needs them, such as draft angles and uniform walls. Then design for the print process: keep walls at a sensible minimum, add radii rather than sharp internal corners, and orient the part so loads run along the layers rather than across them. Build in clearance for the joints and fasteners it will mate with. 76 ADDITIVE reviews designs before printing, so tolerance and orientation problems get caught before a batch is built.
A startup can go from CAD to a field-testable part in days rather than the weeks a tooling cycle takes. That means several design iterations can be tested in a single season, with real feedback from real conditions instead of guesses. Printed parts also let you test complex internal channels and integrated geometries that traditional processes cannot produce at all. 76 ADDITIVE supports end-to-end design and development, so a small team can move from concept to tested component without building a manufacturing function first.
Opening Hours (our printers run through the night)
Monday - Friday, 9am - 5pm


76 Additive
19 Hall Barn Road Industrial Estate
Isleham, Ely
Cambridgeshire, CB7 5RJ
76 Projects t/a 76 Additive
Registered in England & Wales Company no: 10235633
VAT: 245 830 796